Choosing the right Bottom Cover Tape in 2026 requires more than comparing price, width, or adhesive strength. Carrier tape protects sensitive components during feeding, transport, and automated placement. A weak seal can expose pockets to dust, moisture, or vibration. A seal that is too strong can slow peeling and disturb high-speed pick-and-place equipment.
SEMI’s World Fab Forecast continues to show strong investment in semiconductor manufacturing capacity. Smithers’ electronic packaging reports also identify miniaturization, automation, and higher reliability requirements as major market pressures. These trends make tape performance increasingly important, even when the tape appears insignificant. The details matter. Peel force, sealing temperature, antistatic behavior, optical clarity, and storage stability should be checked against the carrier material and machine settings. EIA-481 requirements provide a useful reference, but they cannot replace production trials.
Dr. John H. Lau, a widely published semiconductor packaging specialist, repeatedly emphasizes controlling stress, moisture, and process variation before reliability problems appear. His practical message can be expressed simply: “Control variation before it becomes failure.” That principle applies directly to Bottom Cover Tape selection. A supplier’s datasheet is only a starting point. Ask for peel-force curves, lot-to-lot records, aging results, and compatibility evidence. Test the tape on your actual line. At 25°C, a result may look perfect. At higher speed, humidity, or longer storage, performance can change. There is no universal best tape. The careful choice is the one that remains stable when conditions become less convenient.
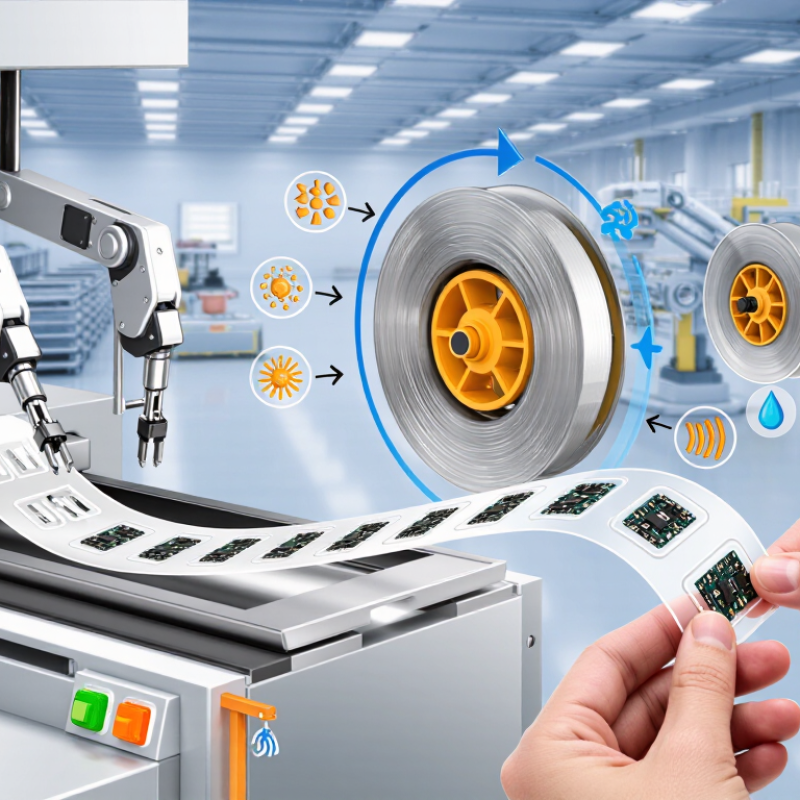
2026 How to Choose the Right Bottom Cover Tape?
What Is Bottom Cover Tape and Why Does It Matter?
Bottom cover tape is a protective adhesive layer applied beneath packaged components, trays, or reel systems. It helps hold parts in position and shields them from dust, abrasion, and handling damage. In electronic packaging, the tape can also support static-control requirements when its material and surface resistance are properly matched.
Its importance becomes clear during transport. A weak adhesive may lift at the edges, while excessive adhesion can damage delicate surfaces during removal. Temperature, humidity, storage time, and sealing pressure also affect performance. In practical production trials, a tape may look secure at room temperature but fail after repeated heating and cooling. That detail is easy to miss.
Choosing the right tape requires more than checking width and price. Review the substrate, adhesive type, peel strength, thickness, and operating temperature. Confirm compatibility with automated equipment and the packaged material. A clean seal is not always a good seal. Sometimes, stronger adhesion creates more problems. The better choice is usually the most stable one, not the most aggressive.
Tips: Test samples under real line conditions. Check edge lifting after storage. Measure peel force consistently. Ask for technical data and batch information. If results vary, repeat the test before approving the tape. Small differences can matter.
| Selection Dimension | What Bottom Cover Tape Does | Common Options or Ranges | Why It Matters | Practical Selection Guidance |
|---|---|---|---|---|
| Primary function | Seals the underside of a carrier-tape pocket and helps retain components during handling, transport, and automated feeding. | Plain protective film; heat-sealable film; antistatic or conductive film. | The tape must protect the part without interfering with pocket formation, indexing, or component pickup. | Confirm whether the application requires sealing only, electrostatic protection, moisture protection, or a combination of these functions. |
| Carrier-tape compatibility | Provides the sealing interface with paper, polystyrene, polycarbonate, or other carrier-tape constructions. | Paper carrier; PS carrier; PC carrier; multilayer polymer carrier. | Different carrier surfaces require different seal temperatures, dwell times, and adhesive or coating systems. | Request compatibility data for the exact carrier material and validate sealing on the actual production line. |
| Tape width | Covers the sealing area across the bottom of the carrier tape while maintaining alignment with the tape path. | Common widths include 8, 12, 16, 24, 32, 44, 56, and 72 mm; other widths may be available. | Incorrect width can cause incomplete sealing, edge lift, excessive material use, or interference with sprocket holes. | Match the cover tape width to the carrier-tape design and keep the tape centered over the intended sealing land. |
| Thickness | Contributes to stiffness, tear resistance, sealing behavior, and the total package profile. | Often selected in the approximate range of 25–100 µm, depending on construction and application. | A thinner film can reduce material use, while a thicker film may improve handling and mechanical protection. | Choose the minimum thickness that passes seal, transport, winding, and feeder-performance tests. |
| Base-film material | Acts as the mechanical support layer and determines much of the tape’s flexibility, strength, and thermal response. | Polyester (PET); polypropylene (PP); polyethylene (PE); multilayer film structures. | Material choice affects tear resistance, dimensional stability, transparency, sealing temperature, and recyclability. | Select a film structure that remains stable at the specified sealing temperature and does not contaminate the component or carrier. |
| Sealing method | Creates a bond between the cover tape and the carrier tape to keep components inside the pockets. | Heat sealing; pressure-sensitive sealing; carrier-specific coated systems. | The sealing method determines equipment requirements, process window, seal uniformity, and opening behavior. | Use the sealing system recommended for the carrier material and verify performance at line speed, not only in laboratory conditions. |
| Seal temperature | Controls activation and flow of the heat-sealable layer when heat sealing is used. | Many heat-seal systems operate broadly around 100–180 °C, but the exact range is construction-specific. | Too little heat may cause weak or intermittent seals; too much heat may deform the carrier or damage sensitive components. | Follow the supplier’s process window and optimize temperature together with pressure, dwell time, and line speed. |
| Peel force and opening profile | Balances component retention during logistics with clean, controlled opening at the placement machine. | Low-, medium-, or high-peel constructions; target values must be established by application testing. | Excessive peel force can cause feeder stoppages or component movement; insufficient force can allow tape lifting or part loss. | Specify a consistent peel profile and measure it using a defined test method, angle, speed, and seal condition. |
| Antistatic or ESD performance | Helps reduce electrostatic charge generation or provides a controlled path for charge dissipation. | Antistatic, dissipative, or conductive constructions; surface resistance depends on the product design. | Static charge can attract dust, disturb lightweight components, or create risk for electrostatic-sensitive devices. | Define the required resistance range and verify the complete packaging system, including carrier, tape, reel, and handling environment. |
| Transparency and inspection | Allows visual or optical inspection of the sealed carrier and its contents when a transparent construction is used. | Clear, translucent, opaque, or printed constructions. | Visibility supports verification of component presence, orientation, contamination, and pocket condition. | Choose transparent tape when inspection is required, provided optical properties do not conflict with ESD or sealing needs. |
| Moisture and environmental protection | Can limit exposure to dust and environmental contaminants, but it is not automatically a moisture-barrier package. | Standard protective film; higher-barrier multilayer structures; moisture-sensitive-device packaging used with sealed bags and desiccant. | Moisture-sensitive components may require packaging controls beyond the bottom cover tape itself. | Treat the tape as one part of the moisture-control system and follow the applicable component-handling requirements. |
| Mechanical strength | Resists tearing, puncture, stretching, and edge damage during winding, shipping, and machine feeding. | Evaluate tensile strength, elongation, tear resistance, puncture resistance, and edge quality. | Mechanical failure can expose components, interrupt feeding, or create loose film fragments. | Test the finished carrier assembly after winding and simulated transport, rather than testing the film alone. |
| Dimensional stability | Maintains alignment and consistent coverage as the sealed carrier passes through the feeder. | Assess shrinkage, curl, width tolerance, thickness tolerance, and roll-winding consistency. | Variation may lead to skewed tape, uneven sealing, sprocket-hole interference, or unstable indexing. | Set dimensional tolerances according to the narrowest part of the packaging and feeding process. |
| Cleanliness and outgassing | Helps prevent particles, adhesive residue, and volatile materials from reaching components or equipment. | Low-particle; low-residue; low-outgassing constructions. | Contamination can affect electrical contacts, optical surfaces, bonding, and feeder reliability. | Request cleanliness specifications and inspect both the tape and sealed carrier under actual production conditions. |
| Quality verification | Confirms that the selected tape performs consistently throughout production and distribution. | Seal-strength testing; peel-force testing; ESD testing; dimensional inspection; visual inspection; feeder trials. | A tape that passes one laboratory test may still fail because of process variation, storage conditions, or machine compatibility. | Approve the tape only after testing the complete packaging system at production speed and under expected storage and shipping conditions. |
Check the component’s shape, weight, surface finish, and sensitivity to static, moisture, dust, or abrasion. Measure real pockets.
Drawings can miss production tolerances. Use real parts and carriers to check pocket depth, overlap, and component movement.
Review sealing temperature, dwell time, line speed, peel force, and storage conditions. A warm-room test can mislead you.
Choose gentler contact for sensitive surfaces. Small parts may need stronger retention, but excessive force can leave marks or cause damage.
Record lifted edges, wrinkles, residue, opening behavior, jams, and component movement. Transport simulation matters.
Measure peel consistency, sealing strength, optical clarity, residue, and storage performance across expected temperatures. Appearance alone is weak evidence.
Request current restricted-substance declarations, halogen information, test dates, and lot-level traceability. Old certificates may not reflect current materials.
Compare yield per 1,000 pockets, not roll price alone. Include waste, cleaning, changeovers, rejected parts, and stoppages.
Sometimes, but the calculation is incomplete. A cheaper roll may create jams, residue, or extra cleaning. That shortcut may cost more.
Record failures honestly, even when the tape is not the only cause. Repeat testing with real operators and shipping conditions. Perfect specifications are rare.
Choosing the right Bottom Cover Tape is essential for protecting products, maintaining package integrity, and supporting efficient sealing operations. This guide explains what Bottom Cover Tape is, how it helps shield packaged items from dust, moisture, and handling damage, and why selecting the correct tape can influence product quality and production consistency. The first step is to identify the product type, package structure, storage conditions, and level of protection required.
The article also compares common tape materials, adhesive properties, sealing strength, temperature resistance, and transparency to help match performance with application needs. It highlights the importance of selecting suitable tape width, thickness, and roll dimensions for existing sealing equipment, while also considering application speed and machine compatibility. Finally, readers will learn how to evaluate quality, documentation, regulatory requirements, supplier reliability, and total cost, ensuring that the chosen Bottom Cover Tape delivers dependable performance without creating unnecessary operational expenses.

 YONGJIA Electronic